
Gas distribution networks often reach a stage where replacement becomes necessary while roads, buildings, utilities, and traffic patterns make open excavation increasingly disruptive. PE pipe extrusion line technology becomes relevant to this challenge because rehabilitation projects require pipes with carefully controlled dimensions and material performance, not simply higher output.
PE100-RC has attracted particular attention in trenchless work because its crack-resistance characteristics can support installation methods that expose the pipe to demanding mechanical conditions. DEKUMA develops extrusion equipment for PE and other thermoplastic pipe applications, providing a manufacturing context for understanding how production requirements change when conventional gas pipe is intended for trenchless rehabilitation.
Why PE100-RC Changes Rehabilitation Specifications
Conventional PE100 gas pipe and PE100-RC pipe share the same basic polyethylene family, but their intended performance envelope is not identical. Standard PE100 distribution pipe is designed around pressure service, dimensional requirements, material classification, and resistance to long-term failure. PE100-RC adds particular emphasis on resistance to slow crack growth, which becomes significant when the pipe encounters localized stresses during installation or operation.
That distinction matters because trenchless rehabilitation does not always provide the clean installation environment available in a newly excavated trench. Existing ground conditions, localized imperfections, installation forces, and contact with surrounding materials can affect the new pipe. PE100+ guidance identifies PE100 and PE100-RC as materials used in pipe bursting, splitting, slip lining, and close-fit lining applications.
Material selection still cannot be separated from structural design. ISO 11295-based rehabilitation guidance distinguishes different lining classes according to the extent to which the new liner must withstand internal pressure and external loading. The appropriate wall thickness, SDR, liner diameter, and host-pipe condition must be established from the actual rehabilitation scenario rather than selected solely because a pipe carries the PE100-RC designation.
Pipe Bursting and Close-Fit Lining
Pipe bursting follows a different logic from conventional replacement. The existing pipeline is fractured or displaced while the replacement PE pipe is pulled through the same general alignment, allowing rehabilitation to proceed without physically removing the old pipe. PE100+ describes both pipe bursting and pipe splitting as trenchless methods capable of using PE100 or PE100-RC replacement pipe.
Mechanical conditions during installation are central to material selection. Pulling forces, localized contact, ground interaction, and the condition of the existing route can create stresses that would be less relevant in an open trench. Crack-resistance becomes especially useful where the installation environment may expose the replacement pipe to concentrated mechanical effects, although project design still needs to consider pipe dimensions, installation loads, operating pressure, and applicable standards.
Close-fit lining works differently. The PE liner is temporarily reduced or deformed so that it can pass through the existing host pipe, after which it returns toward its original geometry. PE100+ explains that the memory characteristics of polyethylene make several close-fit techniques possible, including die drawing, roller reduction, and fold-and-form systems.
Production Controls for Trenchless PE Pipe
The manufacturing process has to accommodate more than resin melting and throughput when pipe will later undergo deformation, pulling, or insertion. Wall thickness, outside diameter, ovality, cooling behavior, and surface condition all influence whether the finished pipe matches the design assumptions used during rehabilitation. Variations that appear minor during factory inspection can become more consequential when the pipe must pass through a restricted host pipeline.
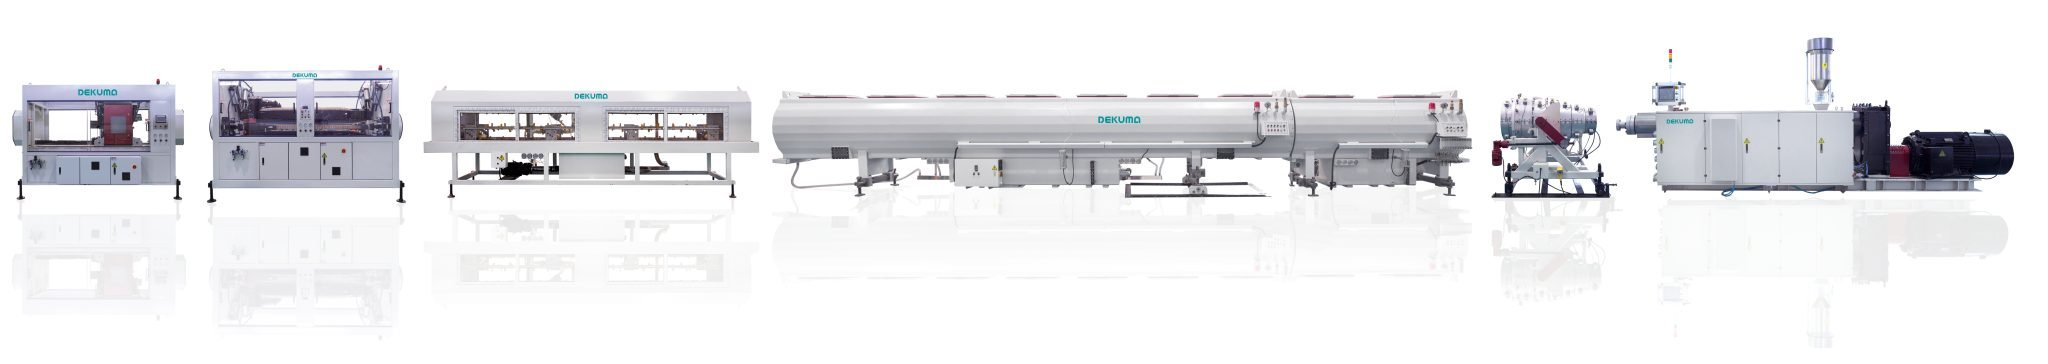
The PE Pipe Extrusion Line supplied by DEKUMA supports PE and HDPE pipe production, with its single-screw extrusion systems covering screw diameters from 45 mm to 150 mm and pipe applications ranging from 5 mm to 2800 mm. The company also specifies Siemens or B&R control systems, real-time data monitoring, vacuum calibration, and precise temperature control within its extrusion solutions. Such equipment characteristics are relevant when manufacturers need stable dimensional control across different pipe specifications.
A PE extruder also needs to accommodate the processing behavior of the selected material grade rather than treating every polyethylene formulation identically. Screw geometry, melt temperature, residence time, cooling conditions, and downstream haul-off settings can affect the final pipe structure. For trenchless products, production records become particularly useful because they connect material batches and processing conditions with dimensional and quality inspections performed on the finished pipe.
From Factory Qualification to Field Installation
Factory production is only one part of rehabilitation performance. Host-pipe inspection remains important because close-fit methods depend on the actual internal geometry of the existing pipeline. PE100+ guidance notes that sections with smaller-than-assumed internal diameters should be identified and located, since local restrictions can interfere with liner reversion.
Dimensional compatibility also affects connection design. Close-fit methods may result in a final liner dimension that differs from the original standard pipe geometry, particularly when deformation and recovery are part of the installation process. PE100+ notes that specialized or expanded fittings can be required for certain non-standard dimensions. This means pipe production, installation equipment, host-pipe inspection, and connection engineering should be considered as one technical chain.
Gas rehabilitation projects additionally require the applicable national and project-specific requirements to be checked before production begins. ISO 11299 addresses renovation of underground gas supply networks and includes provisions for different renovation techniques, with requirements applying to both manufactured components and the as-installed system. A pipe specification that looks suitable at the factory can still be inappropriate if its dimensions, installation method, or connection strategy do not correspond with the rehabilitation design.
Conclusion
Trenchless gas rehabilitation changes the question from simply producing pressure pipe to producing pipe whose material behavior, dimensions, and installation characteristics fit an existing underground asset. PE pipe extrusion line technology supports that objective through controlled extrusion, cooling, sizing, and process monitoring, while the final specification must reflect the selected rehabilitation technique and site conditions.
DEKUMA provides PE extrusion systems for construction and infrastructure applications, giving pipe manufacturers a configurable production platform for different polyethylene pipe requirements.
